01
Separate process production from assembly station supply
Prepare the manpower requirement around the actual Jeddah factory route. Process production follows an approved operating instruction for a material or product; assembly joins identified components through defined stations. Describe which route applies, the departments included and the tasks retained by plant employees. A combined factory headcount cannot explain the different receiving requirements of these operations.
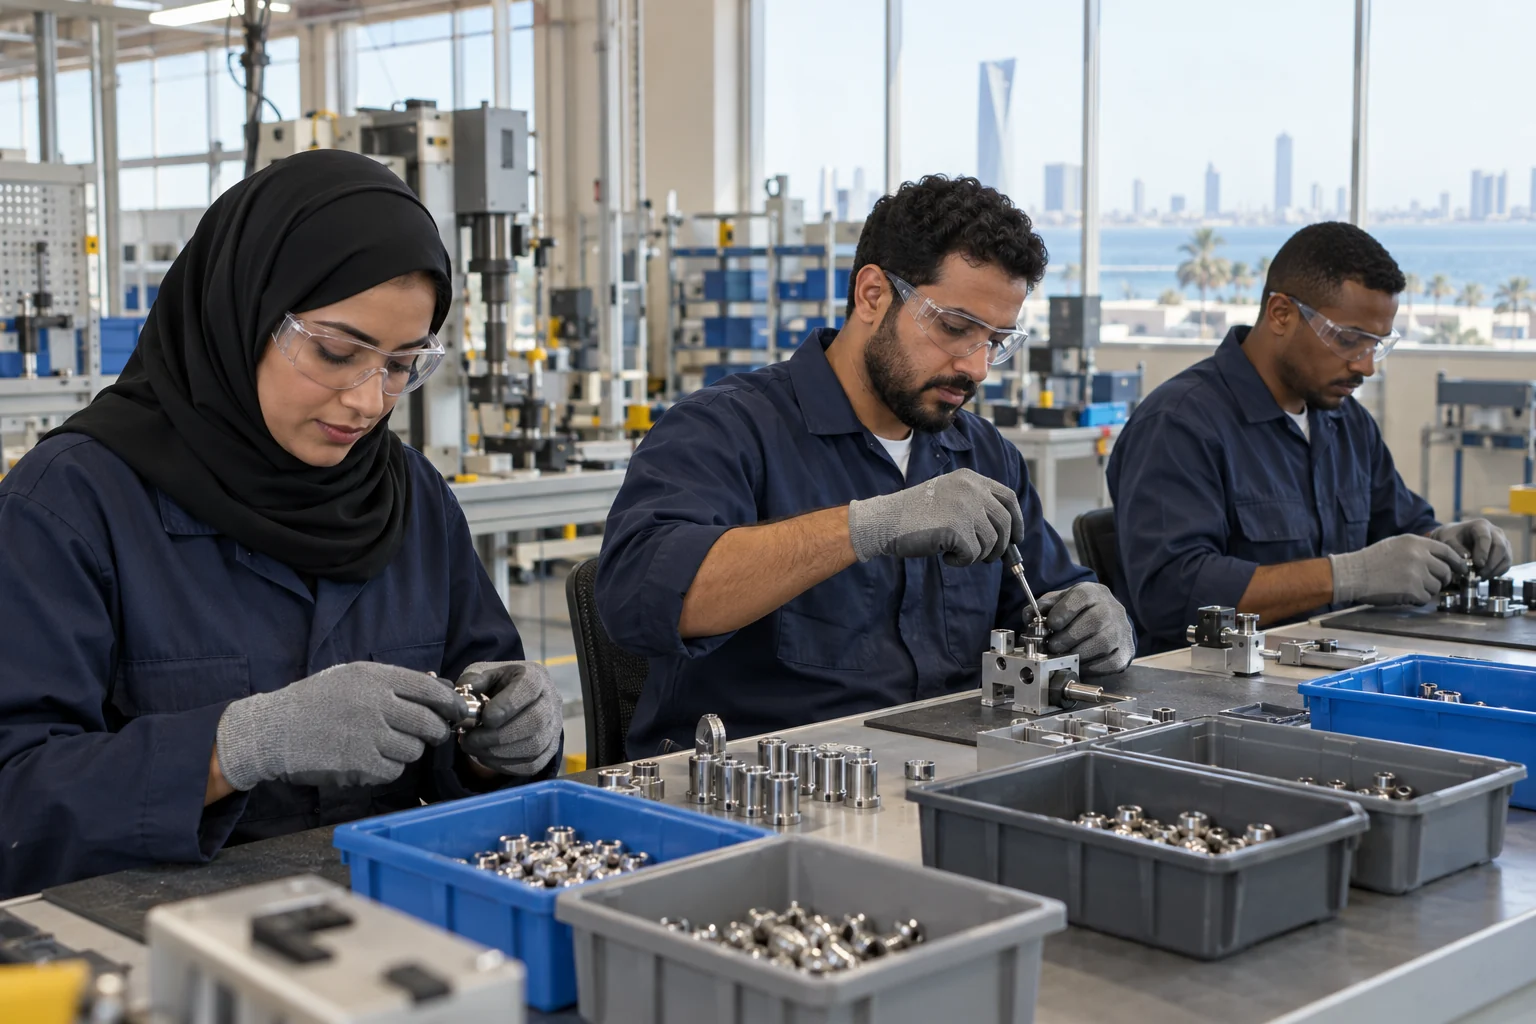
For process production, identify material preparation, allocated equipment operation, checking support and packing where included. For assembly, identify component kitting, assembly stations, inspection support, rework handling and finished-unit packing. Put each assigned team under a named supervisor and state the instruction used at its receiving station.
For a building-materials plant, specify the actual product and departments rather than use construction labour as the factory brief. Identify whether the assignment covers product preparation, fabrication support, finishing, packing or movement to the dispatch area. Include product dimensions, handling equipment and the receiving instruction where relevant to the duties.
02
Plan component kitting before allocating assembly operators
A station can be staffed and still wait for the correct components. Describe the kit reference, component identification, quantities, delivery point and replenishment owner in the supply brief. State whether supplied workers pick from stores, deliver prepared kits or support the station after receipt. Those assignments involve different records and movement responsibilities.
Keep material shortages, conflicting references and incomplete kits visible to the factory owner. Record where the affected kit is held and which station is waiting. A worker assigned to delivery should have an agreed reporting route when identification is unclear; a substitute component requires the designated plant decision. Include that boundary when preparing local instruction.
03
Match station duties to instructions, tools and task evidence
Specify the assembly operation performed at each station, the component family and the relevant tools or fixtures. Describe the prescribed sequence, checks recorded by the worker and handover to the next operation. Allocate skilled execution separately from general component handling so a common operator title does not conceal different competence requirements.
For process equipment, name the equipment family and assigned operating duties in the requirement. Identify who controls settings, technical interventions and release after a stoppage. The receiving supervisor should confirm the current instruction and task readiness before assigning the worker. Supply planning should show the work the person is expected to perform and the decisions retained by the plant.
04
Balance coverage using the factory station sequence
Use the plant’s observed station times and planned operating periods to review coverage. Account for component replenishment, movement between stations, prescribed checks, breaks and handovers. Compare the sequence as a whole: additional people at one station may not increase completed units when another station, material delivery or equipment availability limits the route.
Record planned relief by station and the task evidence required of the relief worker. Where the supervisor proposes a rotation, identify the receiving task and local instruction before changing the allocation. Review waiting time, missing materials and equipment interruptions separately from attendance so a coverage decision addresses the recorded operating cause.
05
Keep inspection, rework and finished-unit handovers traceable
Define which checks assembly workers record, who assesses an exception and who approves the disposition of an affected unit. Identify the work reference and location used to keep units awaiting review separate from the normal station handover. Checking support should have an explicit reporting boundary when the instruction or product reference conflicts.
For rework support, specify the released instruction, assigned task and return point for review. Packing teams need the finished-unit reference, included items, pack quantity and receiving record. The shift handover should identify incomplete units, open component shortages, units awaiting review and the named next owner. This makes the next team’s starting condition clear.
06
Confirm receiving resources and shift ownership
Allocate responsibility for work instructions, tools, fixtures, protective equipment, material access and station supervision. Identify who delivers the local task instruction and who confirms that a worker can receive the assigned station. Record transport and reporting arrangements alongside the work allocation so the factory can distinguish arrival from task readiness.
A shift coordinator needs the station roster, relief allocations, replenishment contacts and handover record. Agree how attendance changes are reported and who approves a reassignment. Review replacement requests against the station duties and evidence required, while recording equipment, material and quality dependencies under their respective factory owners.
07
Send an assembly or process manpower supply brief
Submit the Jeddah plant location, product route, stations included, role quantities by operating period and assignment duration. Add component or material context, equipment families, tool requirements, supervision, relief and the station evidence needed. Identify the target receiving window and the responsibilities the factory retains for instructions, technical decisions and product acceptance.
Use AL AHAD GROUP’s linked business enquiry to request review of this defined supply scope. Compare the response with the station allocation, receiving resources and agreed operating responsibilities. If the requirement is to recruit individual factory employees, use the corresponding agency guide and approve a separate position profile and selection process for each appointment.