01
Map each line position
List the workstations, permitted actions, expected material flow and handoff to the next position. State whether roles rotate and which stations require additional experience or authorization.
Use a task sheet for each line position rather than one broad production worker description.
02
Define product and hygiene controls
Identify the product category, controlled area, clothing, hand hygiene, contamination-prevention and material-separation procedures provided by the employer. State prohibited items and the changeover process between products.
Food, pharmaceutical, chemical or other controlled production requires the operator's specific approved procedure and role verification.
03
Set machine and guarding boundaries
Describe whether staff load materials, start or stop a line, clear routine items or only work beside the equipment. Define lockout, jam, guard, alarm and maintenance boundaries.
No worker should bypass a guard, enter a restricted area or repair equipment outside the employer's verified authorization and safe system of work.
- Permitted operating action
- Stop condition
- Supervisor response
- Maintenance handover
04
Document quality checks
List visible checks, count checks, weight or code checks and packing standards assigned to the role. Provide the sample, limit and reporting method controlled by the employer.
Separate recording an observation from approving, releasing or rejecting a production batch unless that authority is expressly assigned.
05
Plan shifts and line handover
Provide shift times, breaks, changeovers, cleaning windows, planned output conditions and relief positions. State how incomplete material, rejects, counts and equipment status transfer to the next shift.
Team leaders and employer line supervision should be shown separately in the requested headcount.
06
Send a line-specific manpower request
Provide the Jeddah facility, product category, line tasks, quantities, shifts, duration and mandatory checks. Confirm transport, meals, uniform, PPE, training, equipment authorization and supervision responsibilities.
Role fit, availability and mobilisation dates are confirmed only after the complete authorized scope is reviewed.
07
Define the station and the next handover
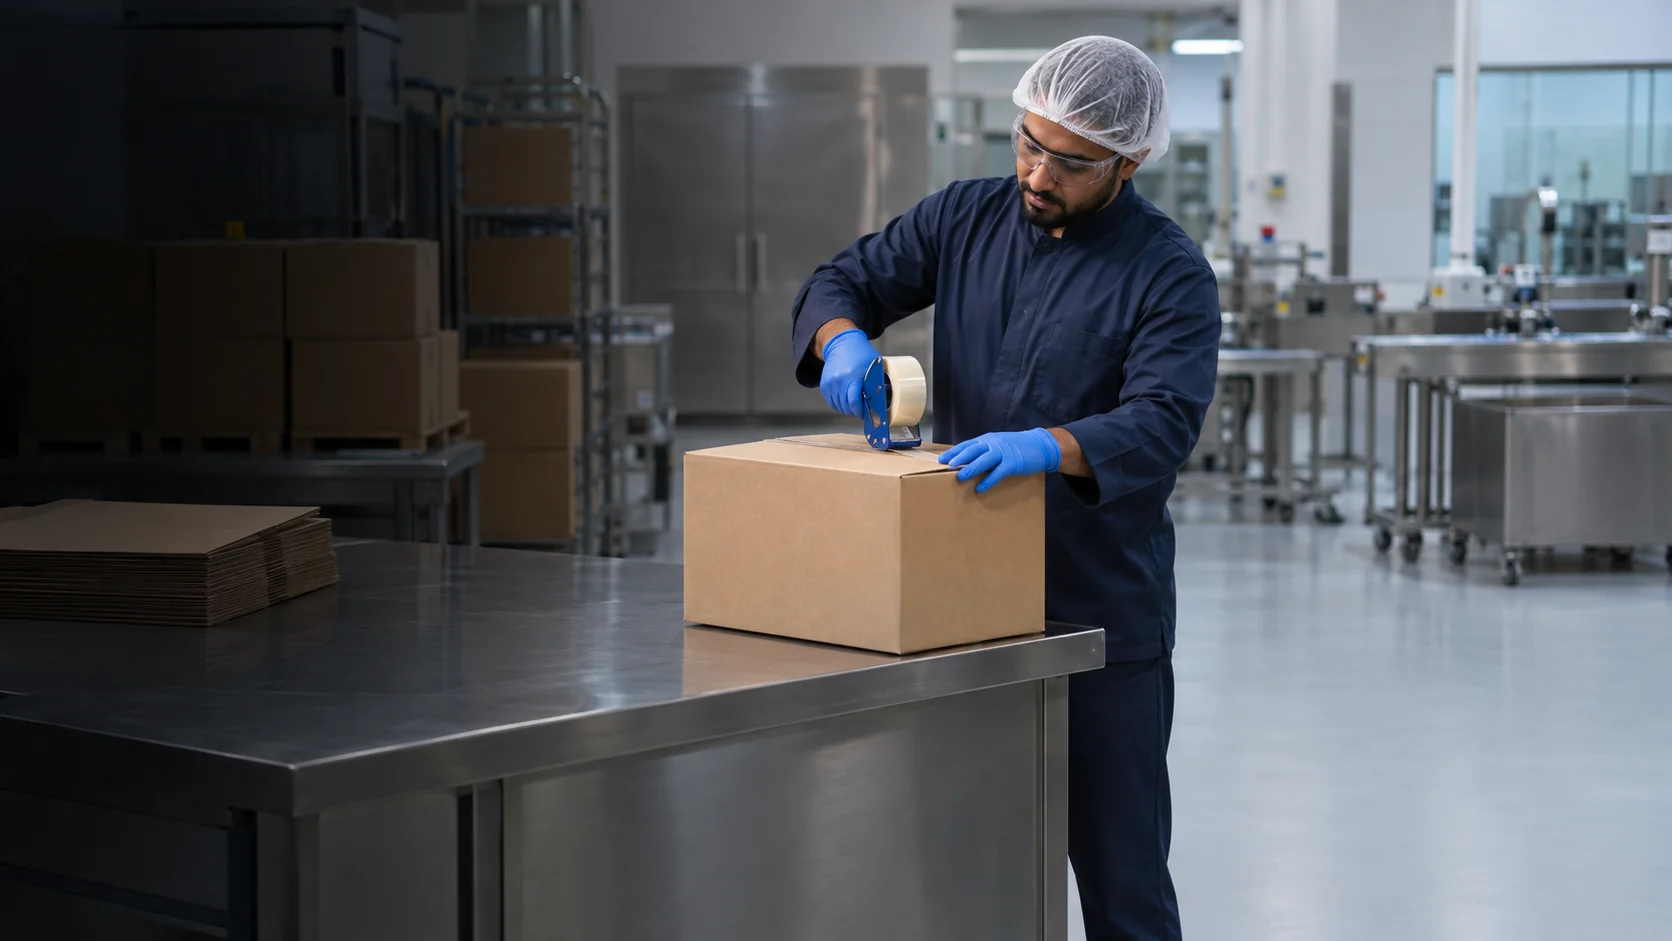
A production or packaging role should identify the product, station, task instruction and receiving station. Separate material preparation, machine operation, manual packing, prescribed checks and finished-product movement. A general production title cannot establish authority to operate every machine or accept every quality decision.
Describe what the worker receives, what they do and what evidence or material they pass onward. Name the supervisor and the owner of release or acceptance decisions. Keep operators, helpers, checkers and material handlers distinguishable in the role schedule.
- Preparation helpers: approved material identity, assigned movement and supply to the station.
- Operators: actual machine, authorized task, instructions and reporting boundaries.
- Packers: item, pack format, quantity, label instruction and downstream handover.
- Checking staff: prescribed observations, records and escalation to the acceptance owner.
- Line supervisors: allocation, station interfaces and next-shift exception ownership.
08
Production manpower supply planning at the constrained station
Map the production sequence and identify where workload accumulates. Review the employer’s actual station timings, interruptions, changeovers, material supply and accepted output. Extra packers cannot independently resolve a delay caused by unavailable material or an upstream machine condition.
Separate planned station coverage, relief, replenishment and follow-up work. Record which tasks can be moved and which require a separately reviewed role. Adjust the roster against the actual constraint and approved work sequence rather than applying one headcount figure to every station.
09
Keep prescribed checks separate from product release
Workers performing an assigned check should know what to observe, how to record it and who decides the next action. Describe the treatment of a mismatched label, unclear instruction, damaged pack or observation outside the approved criteria. Use the employer’s product-specific procedure and escalation route.
A completed observation is not automatically a product-release decision. Keep the checker’s record, any rework instruction and the acceptance owner visible. Workers should seek the responsible supervisor’s direction when the task or condition falls outside their authorized scope.
10
Hand over materials, work in progress and unresolved items
At shift change, distinguish issued materials, accepted output, work awaiting a check and items awaiting a supervisor decision. Record the station, product or batch reference used by the employer, current task status and next owner. Keep the handover aligned with the actual production record.
Send the product context, station duties, machine or manual task, shifts, quantities, supervision, essential experience and joining window for review. Confirm instructions, equipment and access responsibilities before assignment. This guide supports manpower supply planning and does not promise production output, worker availability or a confirmed factory deployment.